Description
Core Technology Scope & Treatment Capabilities
Our multi-barrier treatment approach utilizes specialized filtration technologies tailored to your raw wastewater characteristics.
01
Membrane Bio-Reactor (MBR)
Integrates conventional activated sludge treatment with low-pressure membrane separation. Eliminates secondary clarifiers and yields high-clarity effluent.
- Footprint reduced by up to 50%
- Produces low-turbidity feed for RO
- Removes biomass & suspended solids
02
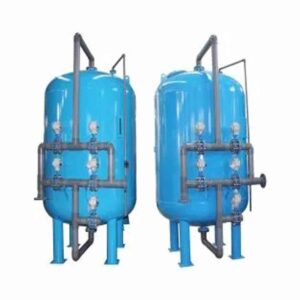
Ultrafiltration (UF)
A pressure-driven separation process removing suspended solids, bacteria, viruses, and macromolecular organic matter down to 0.01–0.1 microns.
- Automated backwash and CIP cycles
- Protects downstream RO systems
- Consistently maintains SDI < 3
03
Submersible UF Filtration (SUF)
Immersed membrane modules operating directly inside high-solids aeration or filtration tanks via low-pressure vacuum suction.
- Low operational energy requirements
- Handles high organic loading rates
- Easy modular capacity expansion
04
Reverse Osmosis (RO)
High-pressure membrane technology designed to separate dissolved inorganic salts, heavy metals, and trace compounds from water.
- Up to 98%+ TDS removal efficiency
- Enables reuse for boilers and cooling towers
- Core driver for ZLD plant layouts
05
Multiple Effect Evaporator (MEE)
A thermal concentration technology that reuses vapor latent heat across multiple stages to evaporate high-salinity RO reject and achieve Zero Liquid Discharge (ZLD).
- High thermal energy efficiency via multi-stage steam reuse
- Converts concentrated brine into reusable condensate water
- Achieves total liquid elimination with dry salt crystal recovery
System Specifications & Purification Flow
| Process Stage | Technology Used | Target Pollutants Removed | Output Quality |
|---|---|---|---|
| Secondary Treatment | MBR / Submersible UF | BOD, COD, Suspended Solids, Pathogens | Clear Effluent (Turbidity < 0.2 NTU) |
| Polishing Stage | Ultrafiltration (UF) | Fine Colloids, Micro-Plastics, Bacteria | SDI < 3 (RO Feed Grade) |
| Desalination & Reuse | Reverse Osmosis (RO) | TDS, Heavy Metals, Dissolved Salts | Process-Grade Reclaimed Water |
| Thermal Evaporation in ZLD | Multiple Effect Evaporator (MEE) | Concentrated RO Brine & High-TDS Residue | Pure Distillate Water & Dry Salt Cake |